CZS Zeman Verschiedene Maschinen
usedVerified seller

1 / 8
Technical data
· ID 169375635Machines
- Net price
- 1.300.000 € netto
- Condition
- used
- Year of manufacture
- 2026
- Location
- 42-20 Czestochowa
Identifikation
ManufacturerCZS
ModelZeman
Technik
Quantity1
Description
The line is from 2010. Modernization done in 2020.
SPECIFICATIONS OF THE ZEMAN CZS LINE
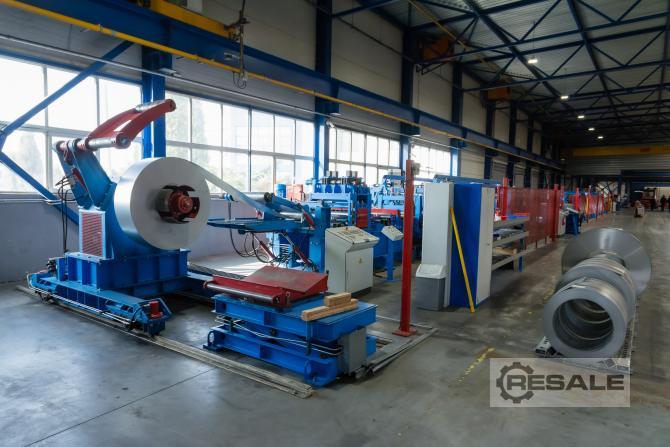
ZEMAN's flagship product, the fully automated "PURLIN" line, is used for the production of open
cold-formed sections such as C, Z and SIGMA, with different widths and shapes, thanks to the fully
automatic adjustment of the profiling rollers. Coils up to 750 wide can be used as raw material
mm and sheet thickness 1.25 mm – 3 mm in grade S-390 and lower. The machine is adapted to
production of elements up to 15 m in length. Width adjustment of specially hardened profiling rollers
It is done steplessly, using only dedicated software. Fully integrated
the "flying punching" device makes all kinds of mounting holes, and the whole process is
continuous, which means that the material does not stop to perform individual operations such as punching
holes or cross-cutting. To maintain production efficiency, the line speed is optimized
dynamically. The machine slows down and accelerates automatically without operator intervention.
Decoiler for sheet metal coils with a permissible working load of 15 tons. Mounted on a walk-through
trolley gives the possibility to accurately center the strip of material before feeding it into the straightener.
Straightener with sickle straightening system allowing the material to be straightened, ensuring
required flatness of the sheet metal and sickle reduction on the feed belt.
2. Punching section
The section contains 5 double, "flying" punching portals, which can be armed with 20 small (up to 40
mm) or 10 large (up to 100 mm) tools (punches and dies) for punching mounting holes.
You can also use a mix of them.
3. Pre-notch guillotine
A "flying" guillotine used to make preliminary holes for the shut-off guillotine. This process has to
The task is to maintain the continuity of the material, thanks to which we obtain a more precise shape of the profile. Especially
its beginning and end. It is an adaptive guillotine that adjusts the width of the hole to the
sheet metal width.
4. Guide carriage/ SIGMA modules
The guide carriage is used to center the sheet metal strip before entering the profiling machine. It is interchangeable
with a module for the production of profiles in the shape of Sigma. If there is a need to produce S+ profiles, it is necessary to
put out a table with a guide and insert two Sigma modules in its place. These modules are positioned in the
It is automatic and independent of the left and right side.
6. Rotary shut-off guillotine.
Rotary shut-off guillotine with hook knives is used to finally cut the section from the belt
material using the holes made by the initial incision guillotine. It is a "flying" guillotine in
Therefore, the sheet metal does not stop for the cutting process. Depending on the profile produced, it is necessary to
Attach the properly oriented cutting cassette.
7. Receiving Table
The receiving table is used to automatically dump the made profiles from the roller conveyor. After which
The elements are manually arranged into a package. The design allows the package to be freely fastened. Table
It is adapted to pick up 15-meter profiles and allows access with a forklift or crane
to pick up a package of sections.
SPECIFICATIONS OF THE ZEMAN CZS LINE
ZEMAN's flagship product, the fully automated "PURLIN" line, is used for the production of open
cold-formed sections such as C, Z and SIGMA, with different widths and shapes, thanks to the fully
automatic adjustment of the profiling rollers. Coils up to 750 wide can be used as raw material
mm and sheet thickness 1.25 mm – 3 mm in grade S-390 and lower. The machine is adapted to
production of elements up to 15 m in length. Width adjustment of specially hardened profiling rollers
It is done steplessly, using only dedicated software. Fully integrated
the "flying punching" device makes all kinds of mounting holes, and the whole process is
continuous, which means that the material does not stop to perform individual operations such as punching
holes or cross-cutting. To maintain production efficiency, the line speed is optimized
dynamically. The machine slows down and accelerates automatically without operator intervention.
Decoiler for sheet metal coils with a permissible working load of 15 tons. Mounted on a walk-through
trolley gives the possibility to accurately center the strip of material before feeding it into the straightener.
Straightener with sickle straightening system allowing the material to be straightened, ensuring
required flatness of the sheet metal and sickle reduction on the feed belt.
2. Punching section
The section contains 5 double, "flying" punching portals, which can be armed with 20 small (up to 40
mm) or 10 large (up to 100 mm) tools (punches and dies) for punching mounting holes.
You can also use a mix of them.
3. Pre-notch guillotine
A "flying" guillotine used to make preliminary holes for the shut-off guillotine. This process has to
The task is to maintain the continuity of the material, thanks to which we obtain a more precise shape of the profile. Especially
its beginning and end. It is an adaptive guillotine that adjusts the width of the hole to the
sheet metal width.
4. Guide carriage/ SIGMA modules
The guide carriage is used to center the sheet metal strip before entering the profiling machine. It is interchangeable
with a module for the production of profiles in the shape of Sigma. If there is a need to produce S+ profiles, it is necessary to
put out a table with a guide and insert two Sigma modules in its place. These modules are positioned in the
It is automatic and independent of the left and right side.
6. Rotary shut-off guillotine.
Rotary shut-off guillotine with hook knives is used to finally cut the section from the belt
material using the holes made by the initial incision guillotine. It is a "flying" guillotine in
Therefore, the sheet metal does not stop for the cutting process. Depending on the profile produced, it is necessary to
Attach the properly oriented cutting cassette.
7. Receiving Table
The receiving table is used to automatically dump the made profiles from the roller conveyor. After which
The elements are manually arranged into a package. The design allows the package to be freely fastened. Table
It is adapted to pick up 15-meter profiles and allows access with a forklift or crane
to pick up a package of sections.
Inquire about this machine
Your inquiry goes directly to the seller of this machine.